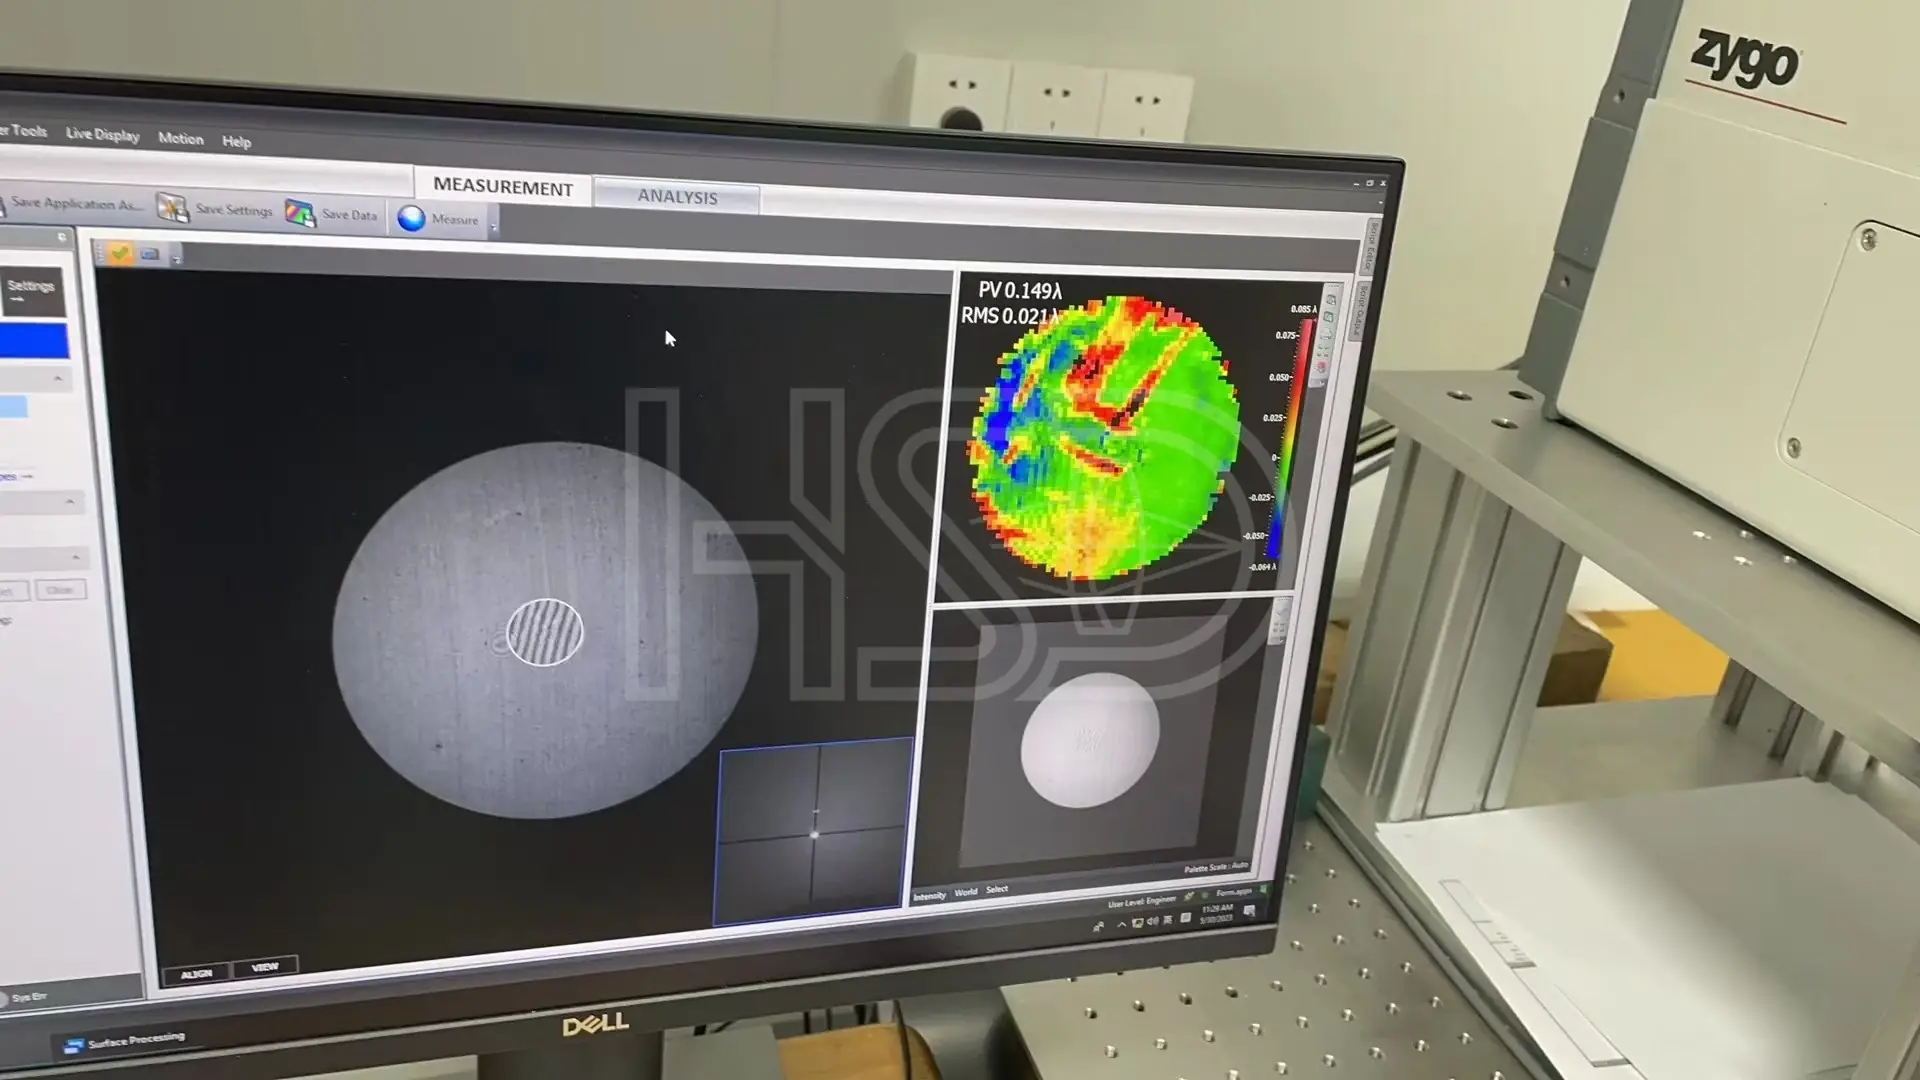
Surface Figure
Surface form tested by interferometry — PV/RMS values from the actual measurement.
Last reviewed: October 2026 · measured values from production batches
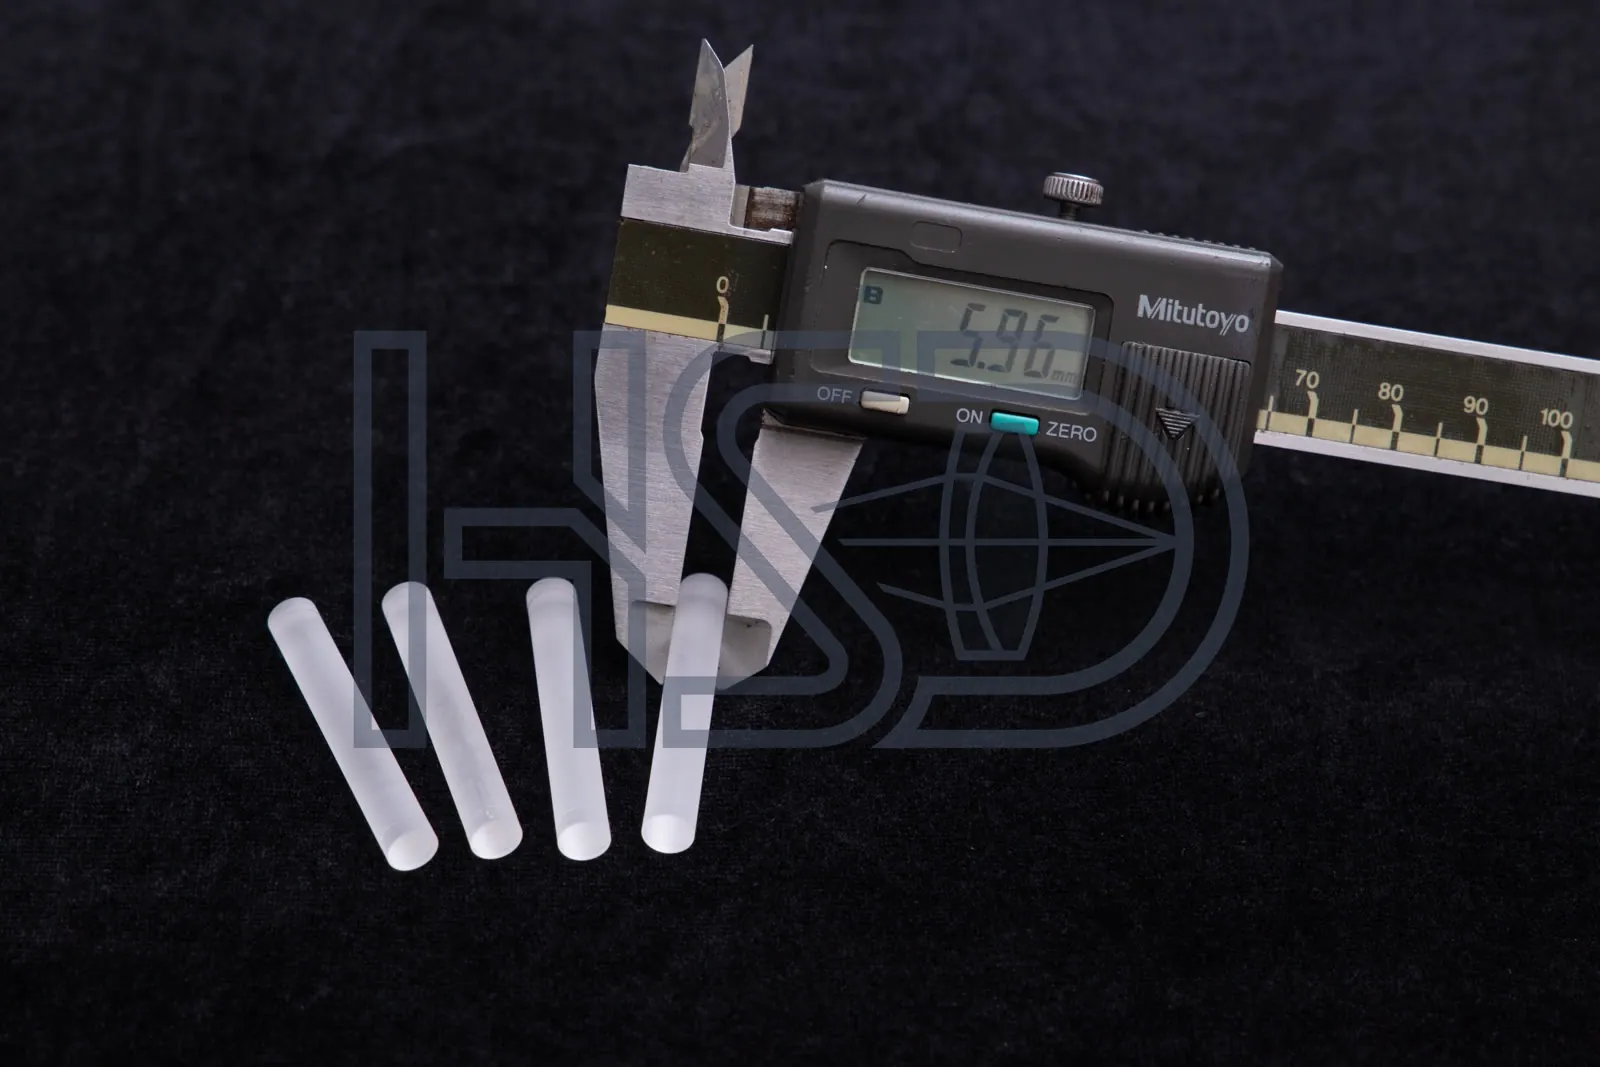
245 standard sizes from 1.19 mm to 8.0 mm OD. Review the size table and send the matching drawing or target dimensions.
Multi-element rod lens assemblies made to print, with cemented groups and batch inspection records.
Nine application pages: arthroscopes, hysteroscopes, cystoscopes, ENT, spine and nephroscopes, industrial borescopes.
Small-diameter relay rods for space-constrained endoscope designs.
Rod lens components for cystoscope relay systems.
Relay rods and assemblies for hysteroscope optical systems.
Rod lens manufacturing for arthroscope OEM programs.
Small-format rod lenses for ENT endoscope assemblies.
Rod lens components for spine and nephroscope relay optics.
Made-to-print rod lenses for industrial inspection optics.
Precision ground blanks for coating laboratories, supplied with measured batch data.
Make-to-print optics for endoscope assemblers, including coated and uncoated options.
These are the standard sizes buyers ask for most often. Each one is made to print with the same diameter tolerance, centration method and batch COA as the rest of the range, and each size page lists the drawing points we confirm before quoting.
Looking for another dimension? The full list of 245 sizes is on the standard rod lens size table. Deutsche Fassung: Standardgrößen für Stablinsen.
1 · Edge softness is an alignment problem. A few arc-minutes of centration error on one rod is magnified through 10–12 relay elements. The image fails at final assembly — at the far end of the train, not at the supplier's inspection bench.
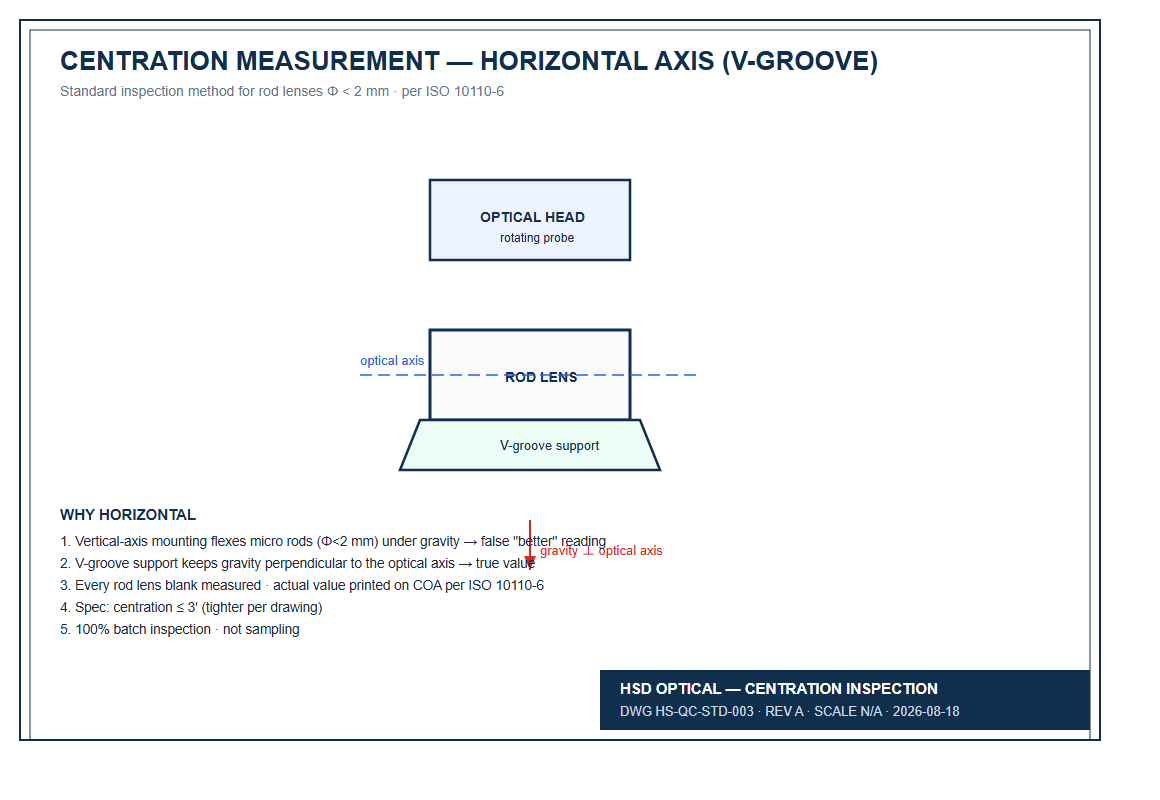
How HSD prevents it: centration is verified on a per-batch sampling plan per ISO 10110-6, with measured values printed on the batch COA before parts leave the factory.
2 · The "manufacturer" may be a reseller. If your supplier outsources to several factories, nobody can explain a yield problem when it appears. The only fix is re-qualifying a second supplier and paying for it twice.
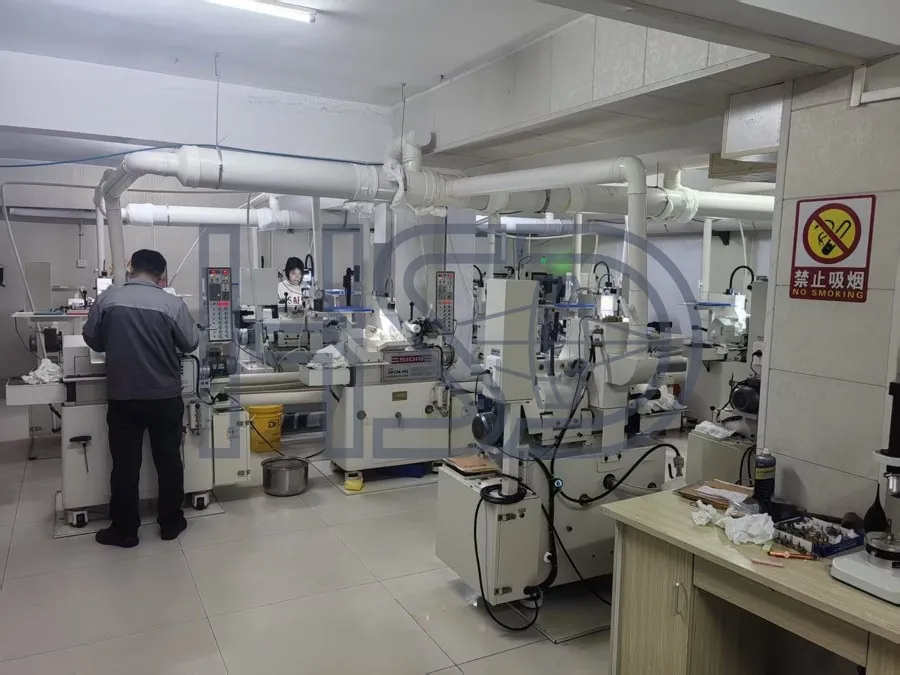
How HSD prevents it: we are the factory — a 30-person precision lens workshop in Nanjing. Your drawing is reviewed by our own engineers, not forwarded to a third party.
3 · Switching mid-production is the most expensive option. Re-qualification, new tooling and delays add up to hundreds of thousands of dollars — and on medical programs, a change can stall the project for months.
How HSD prevents it: your drawing is reviewed engineer-to-engineer before production starts, so the parts that ship match the design you approved — no surprises that force a switch.
4 · Batch drift is invisible until the image tells you. MTF, distortion or centration can shift slightly between lots, pass incoming inspection, and only surface in the assembled scope — where it is almost impossible to trace back to one batch.
How HSD prevents it: every batch COA carries measured values — dimensions, centration, surface quality — so drift is visible at incoming inspection, not at final assembly.
That is why we manufacture a relay train as one system: every element carries the same diameter tolerance, the same centration method and the same COA format — so assembly does not depend on anyone's feel.
| Component | HSD standard range |
|---|---|
| Rod lenses | Φ1.19–8.0 mm · length 10–80 mm · 245 sizes |
| Rear rod lenses | Φ6 class · per drawing |
| Slim relay rods | Φ1.19–1.96 mm · per drawing |
| Uncoated rod lens blanks | For coating labs · per drawing |
| Item | Specification |
|---|---|
| Diameter tolerance | −0.02/−0.04 mm (fit) |
| Length tolerance | Per drawing |
| Centration | ≤3′ (cemented per drawing) · ISO 10110-6 4/3′ |
| Surface quality | 40/20 MIL-PRF-13830B / ISO 10110-7 5/40-20 |
| Edge chipping | ≤0.05 mm, per drawing · ISO 10110-7 E 0.05 |
| Coating | BBAR 400–700 nm R<0.5% |
| Item | Method |
|---|---|
| Centration | Horizontal-axis V-groove · ISO 10110-6 · per-batch sampling inspection |
| COA | 5 lines: part/dims/centration/surface/method |
| Batch | Measured values, not "within spec" |
| Item | Commitment |
|---|---|
| MOQ | 10 pieces |
| Quote | Within 24 h of drawing |
| Confidentiality | NDA standard |
| System | ISO 9001:2015 |
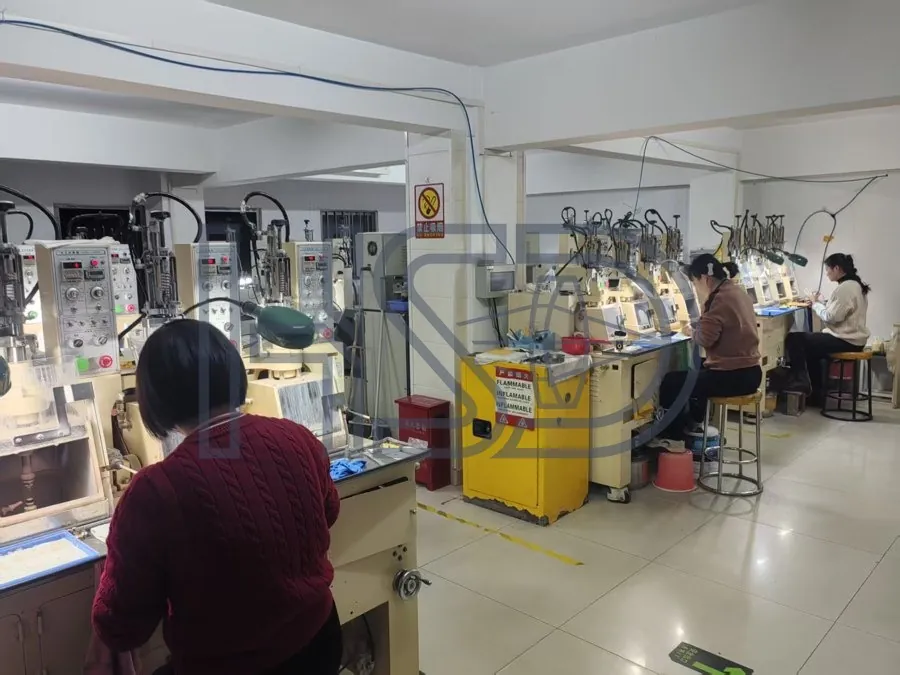
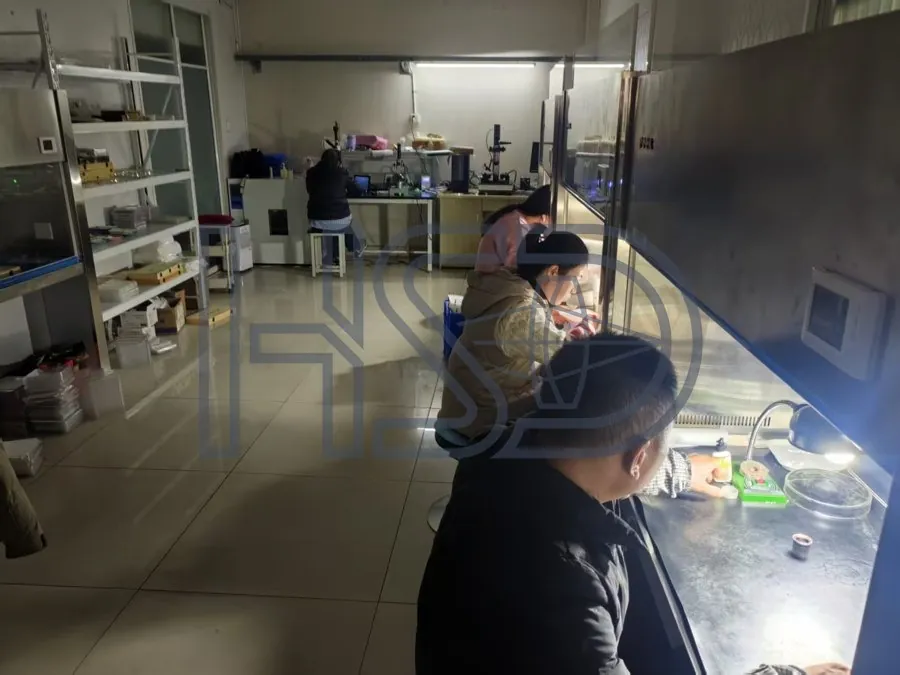
Engineer-to-engineer quote within 24 hours · NDA protected · MOQ 10.
Tell us what you need – quote your drawing number or send the drawing to rfq@hsdoptical.com. Technical review and quotation within 24 hours.
We reply within 24 hours. If you requested an NDA, we send it with our reply.
Inspection & Metrology
Every batch is verified with interferometry, centration measurement and surface inspection. You get the actual measured values, not a “within spec” checkbox.
Surface form tested by interferometry — PV/RMS values from the actual measurement.
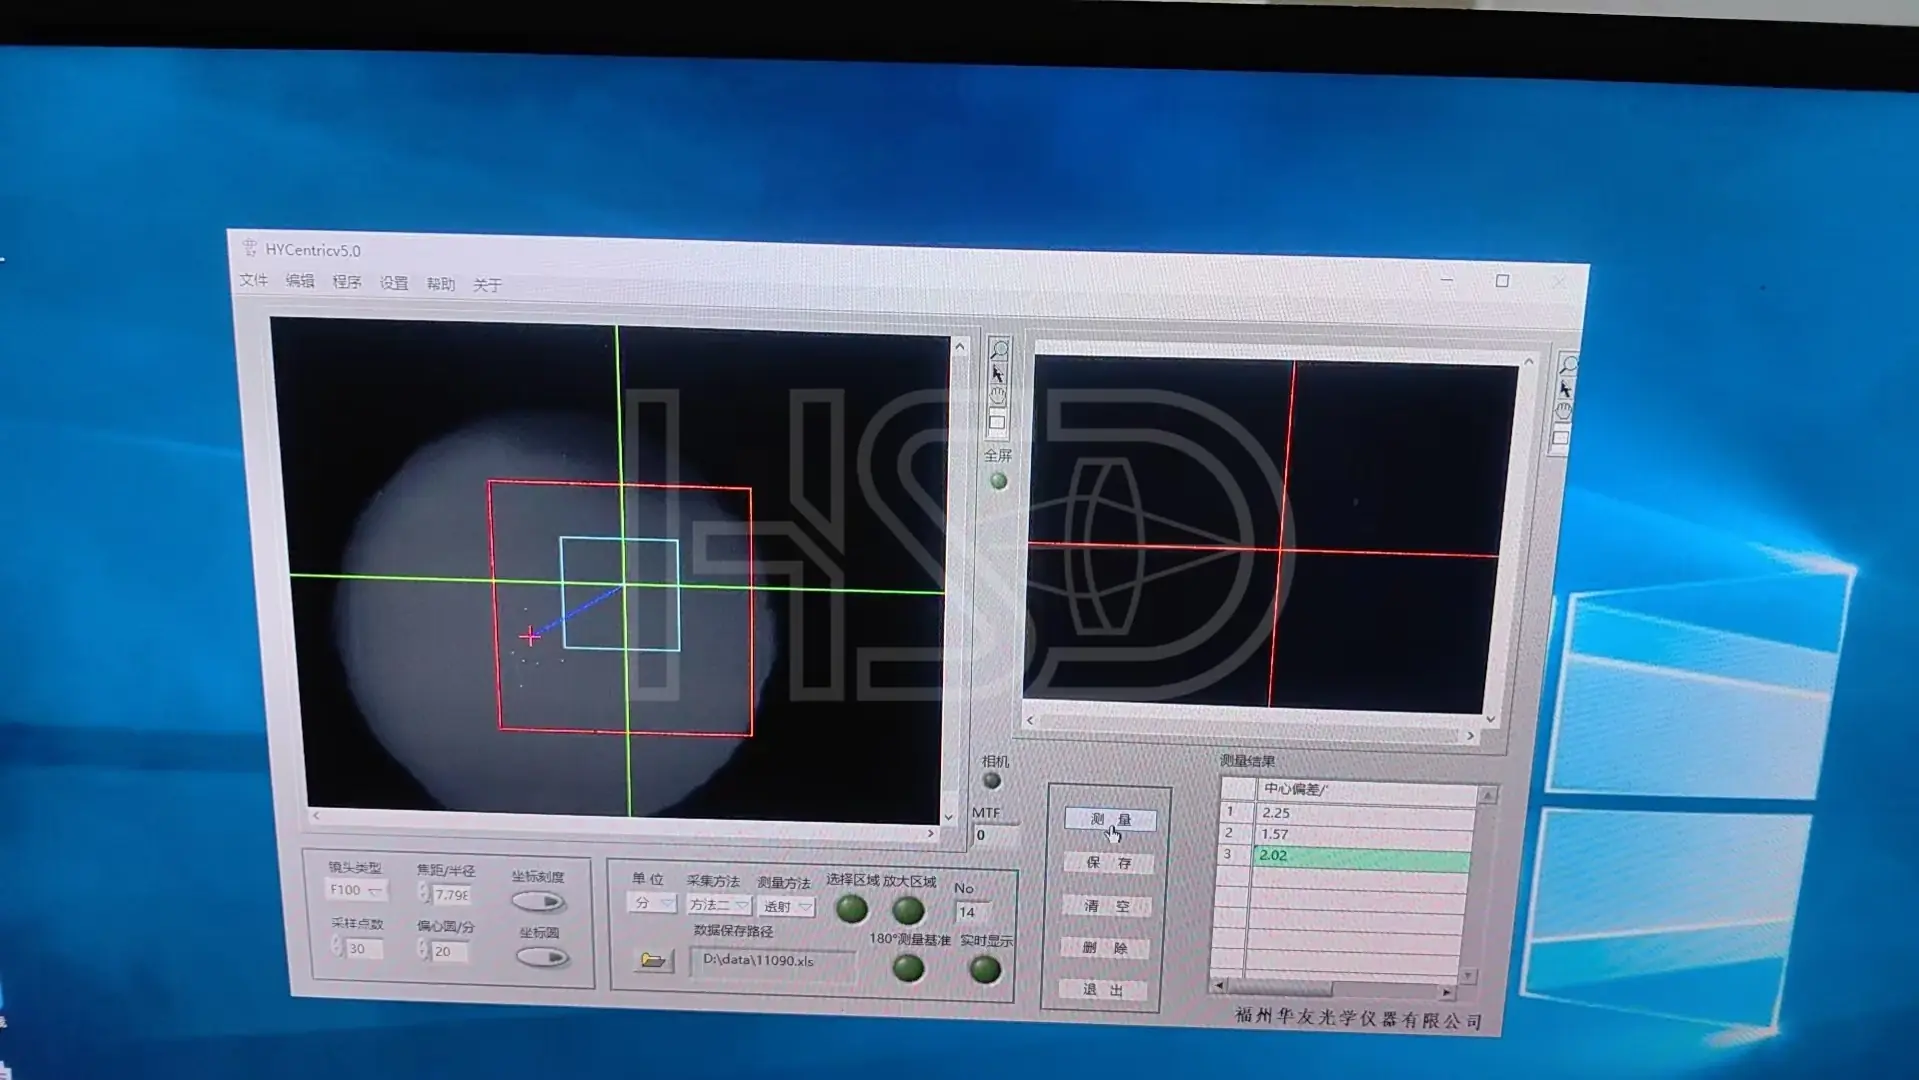
Centration checked on the centration station, typically ≤3′. The reading shown is from a real part — 2.02′.
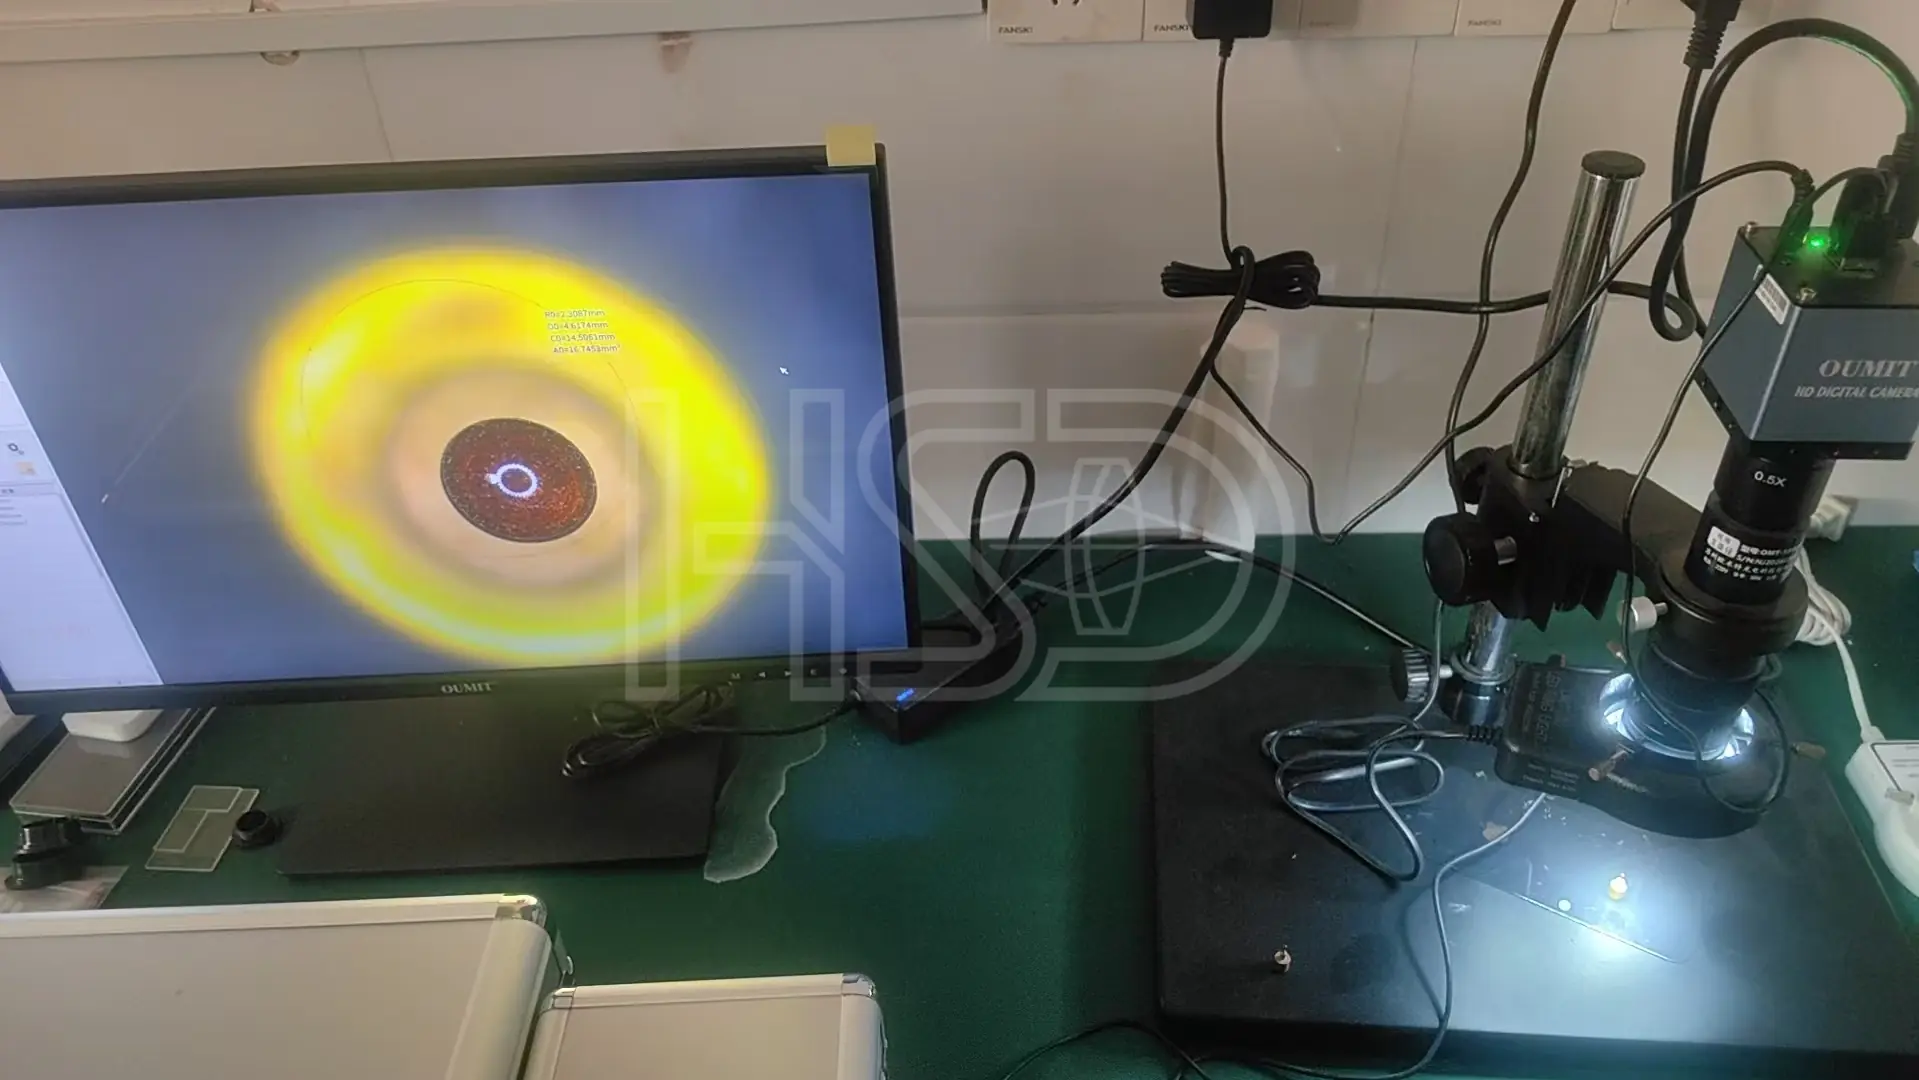
Surface and edge quality inspected under a video microscope — scratch/dig per MIL-PRF-13830B.
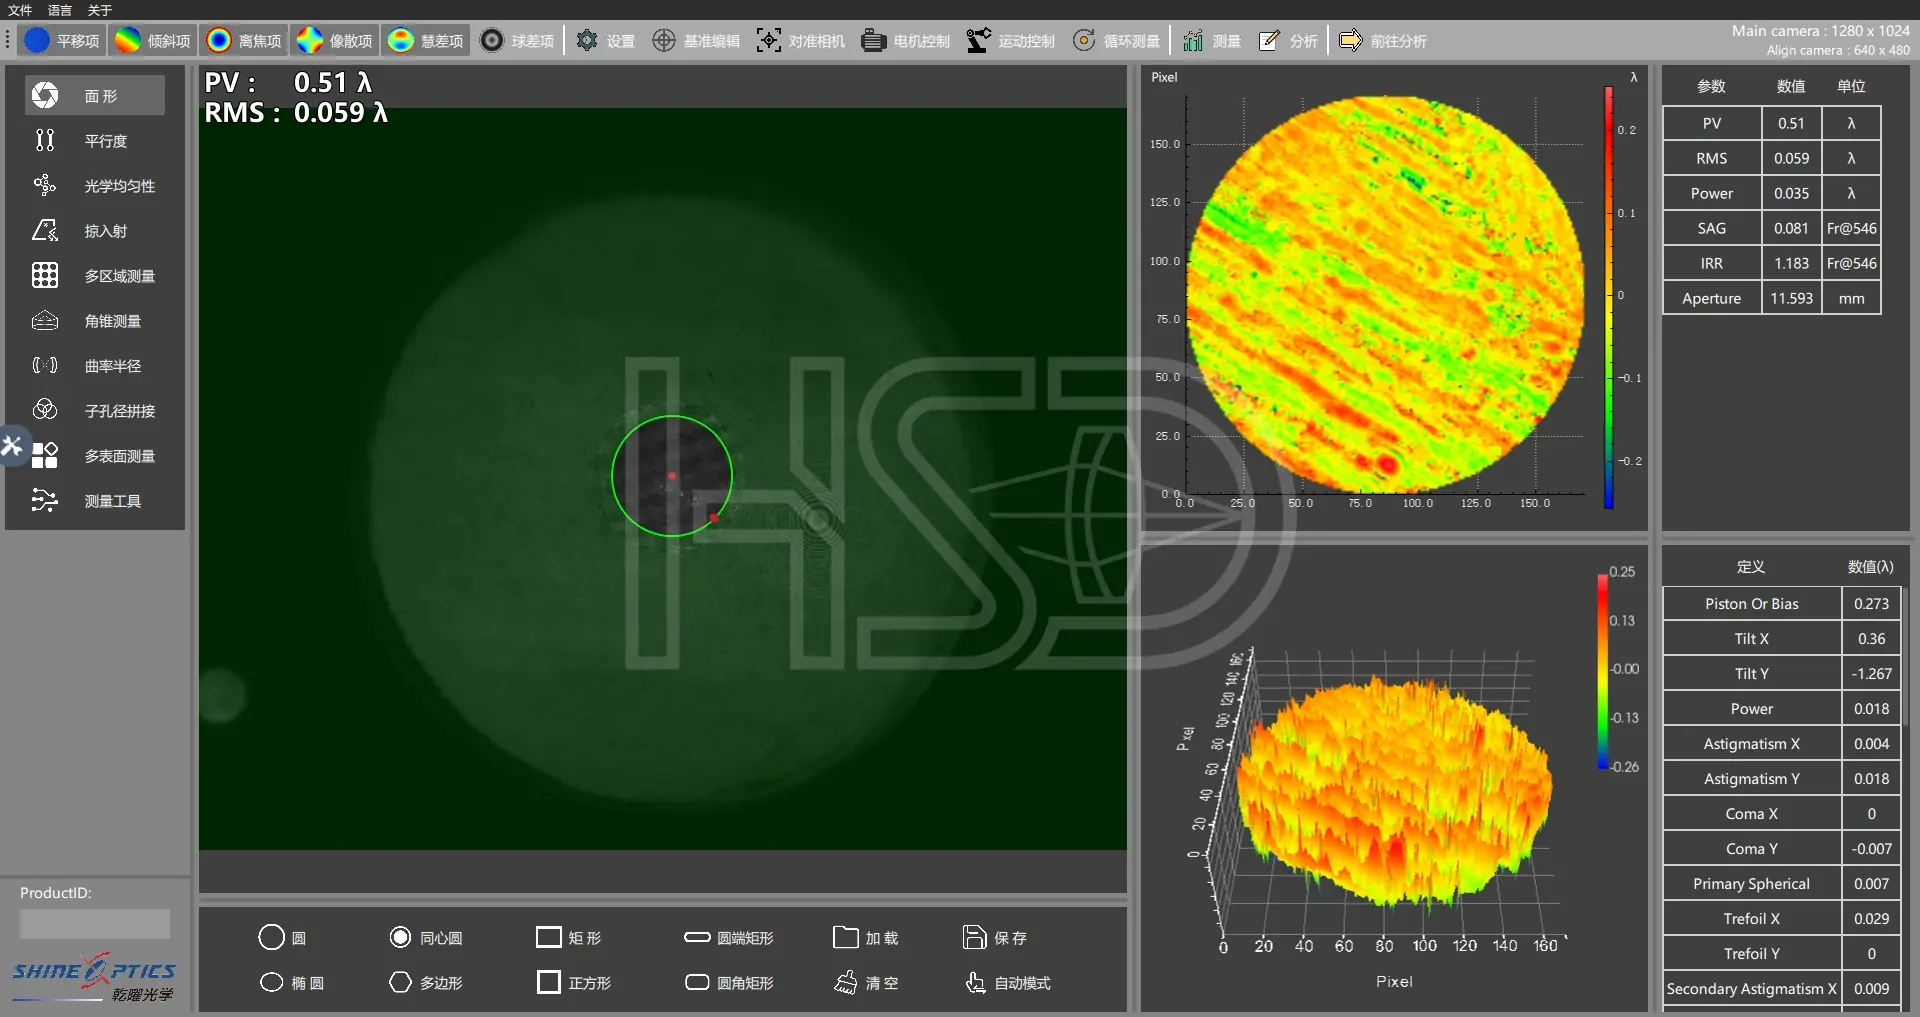
A passing surface from a production run: PV 0.51λ, RMS 0.059λ. Rejects never leave the workshop.
Measured COA per batch — ask for a sample COA with your quote. · Learn how to read a surface map →
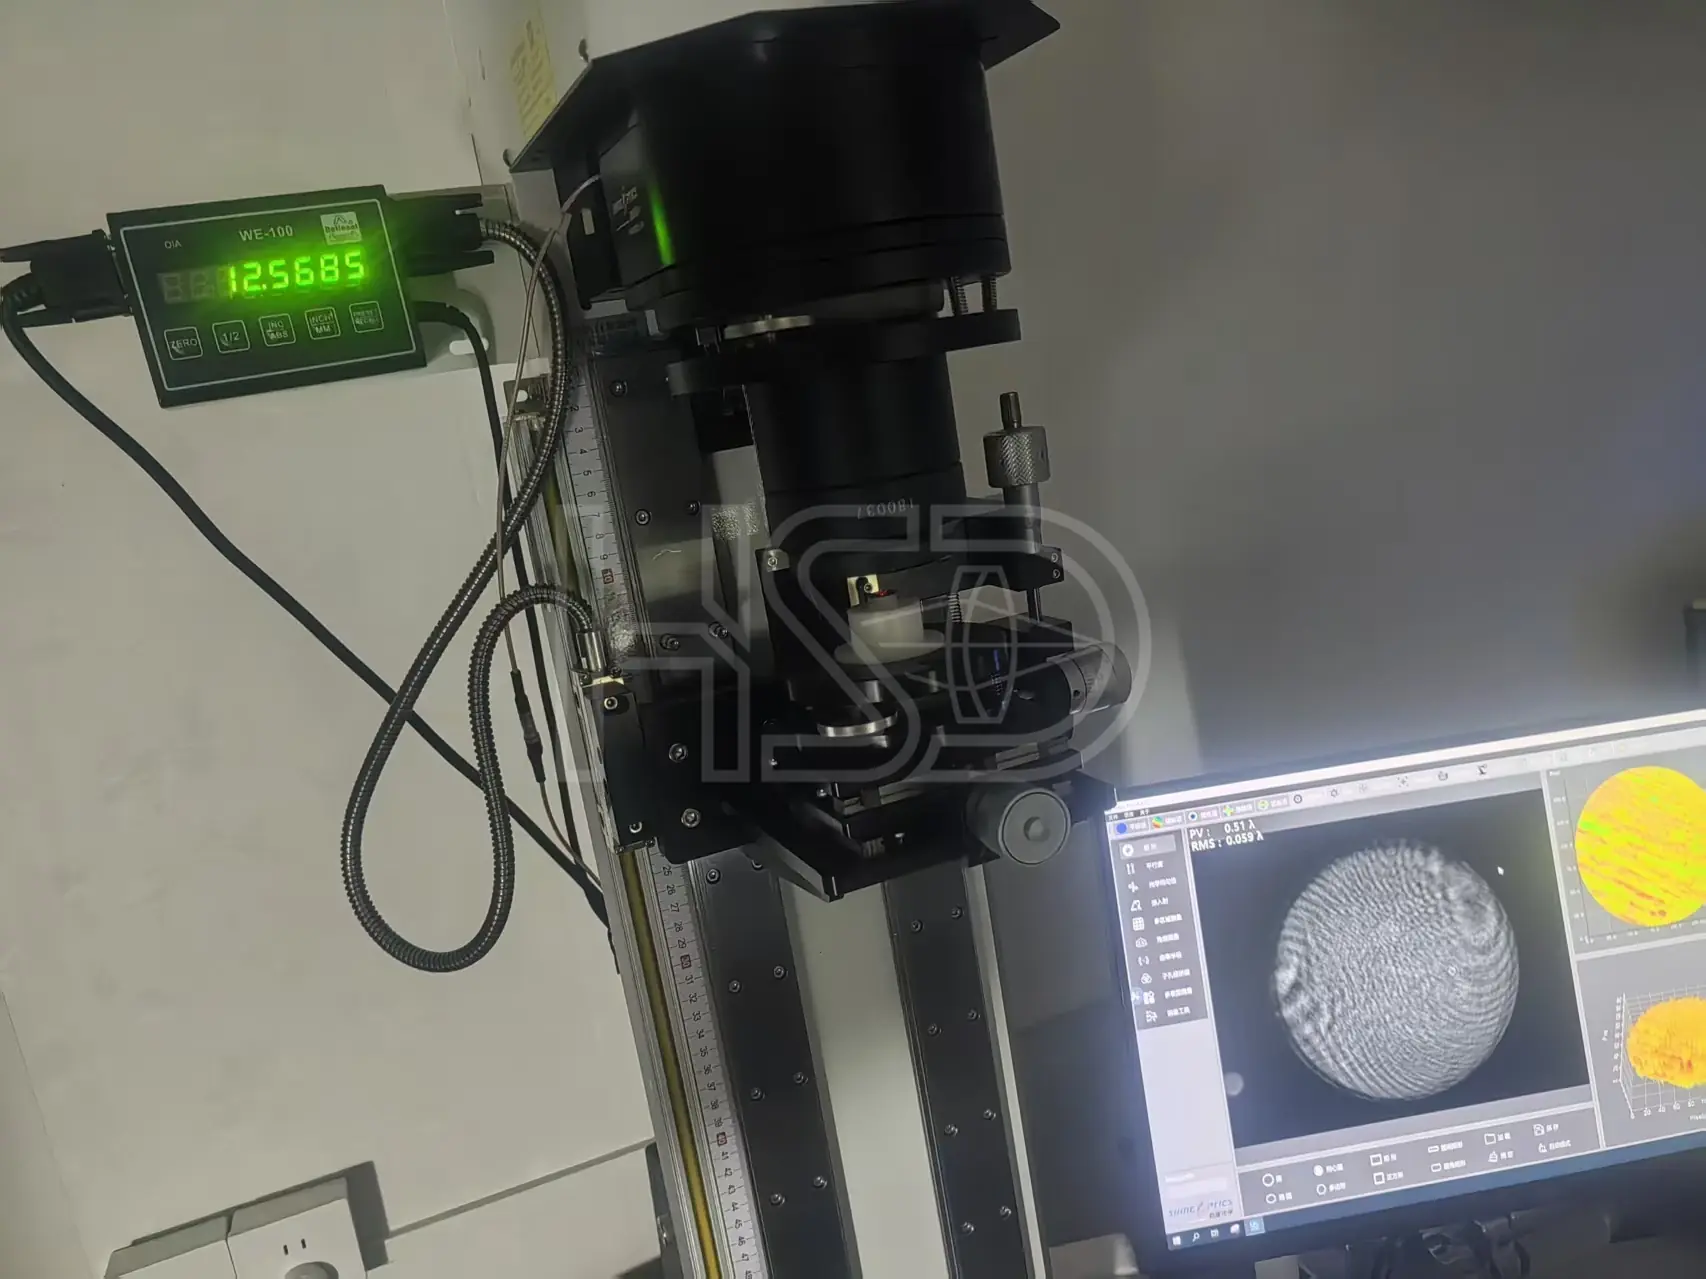
Workstation measurement during rod lens production — PV 0.51λ.
Real measurement, kept on file. Your COA gets the same kind of data.
Watch rod lens grinding, polishing, centration measurement and final inspection in real time. All information shared during the tour is confidential — your NDA is welcome.
Schedule a Live Video Tour