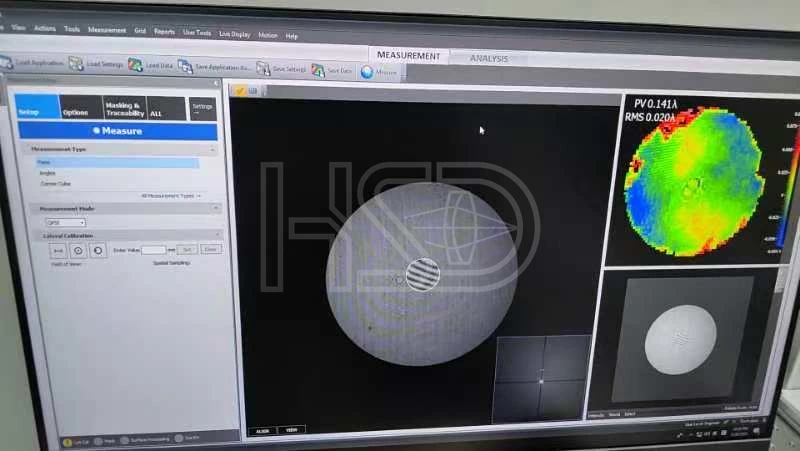
Surface Figure
Surface form tested by interferometry — PV/RMS values from the actual measurement.
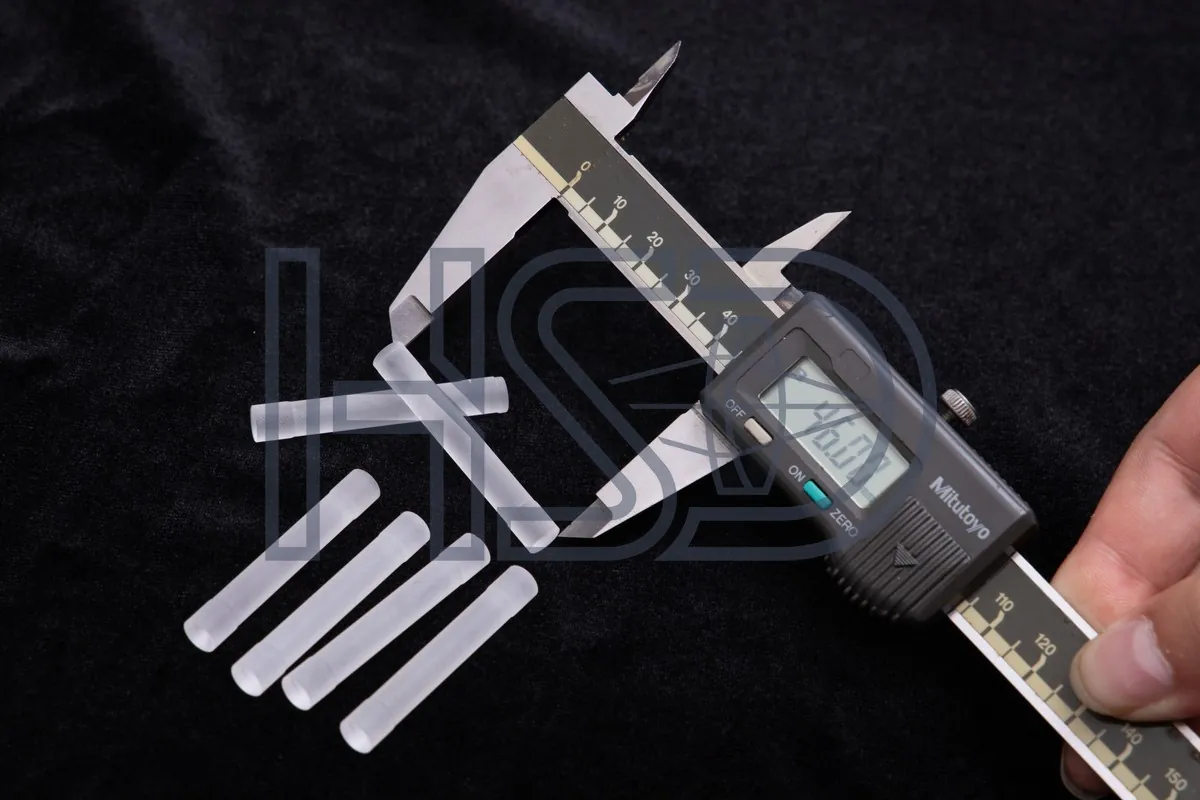
1 · Diameter and length have to be real. A rod 0.02 mm off is invisible to the eye but changes the fit at the coating or assembly stage.
How HSD avoids it: diameter and length are measured per batch; the values go on the COA.
2 · Surface quality carries through. A dig or scratch on a blank survives polishing and shows up in the finished part.
How HSD avoids it: surface is checked to 40/20 MIL-PRF-13830B / ISO 10110-7 5/40-20 before shipment.
3 · Glass grade matters. The grade defines the optical properties — and it has to match the drawing, batch after batch.
How HSD avoids it: material certificates ship with each batch, and we never substitute a grade without written approval.
4 · Consistency between batches is the quiet killer. Rods from different lots can differ more than rods within one lot.
How HSD avoids it: every batch COA carries measured values, so drift is visible before it reaches your line.
A blank is a promise about the finished rod — we keep the measurement on paper.
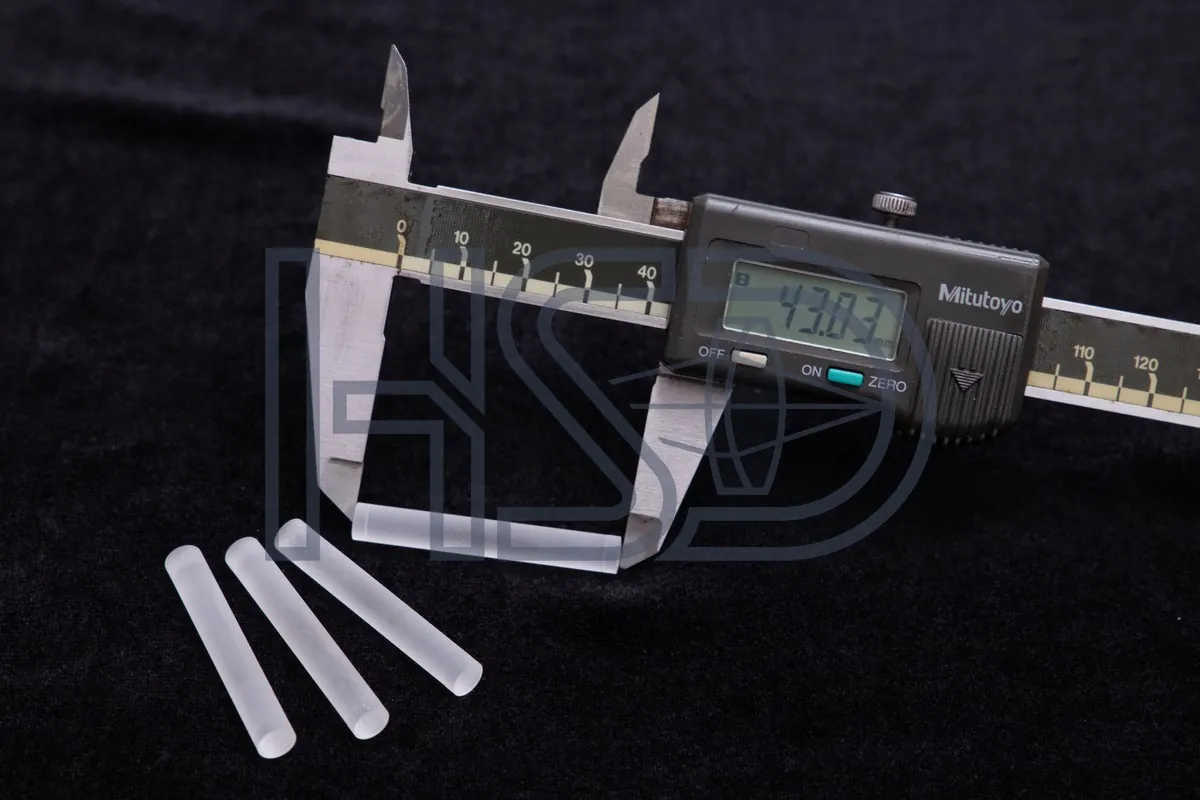
Production photos of long precision glass rods, labeled by length. Final specifications per your drawing.
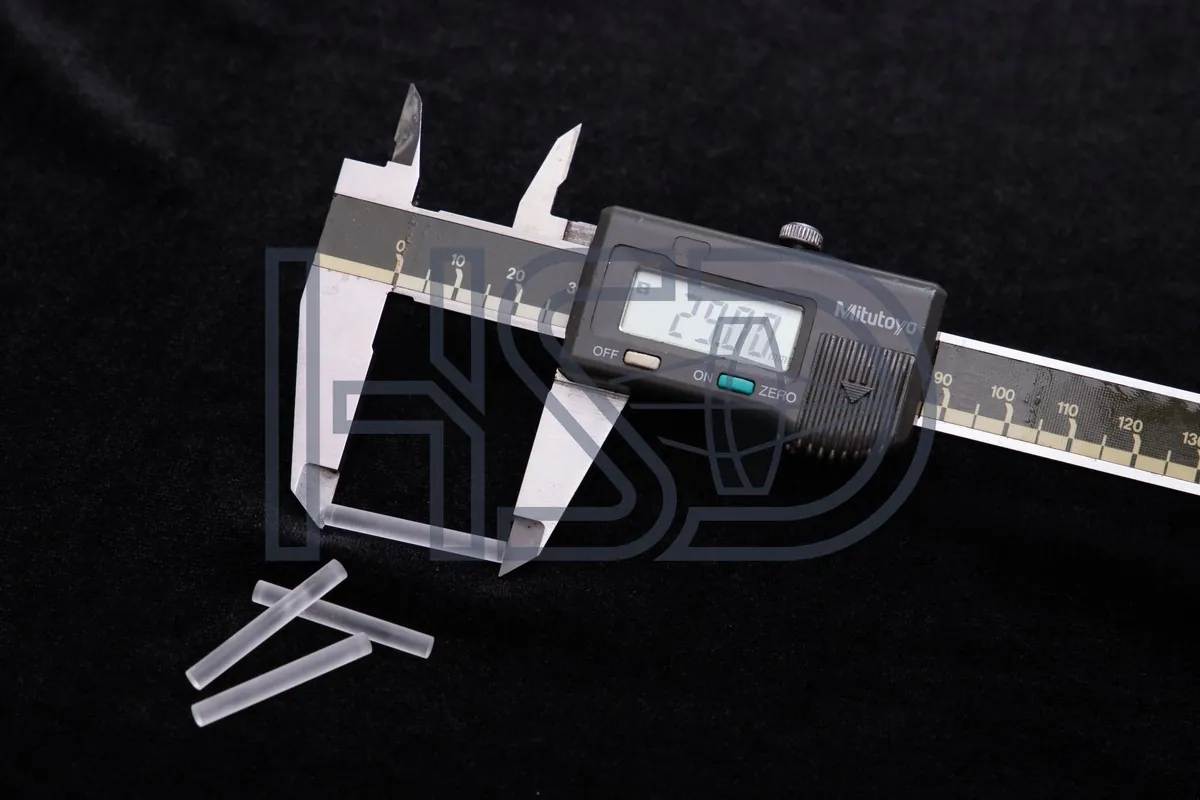
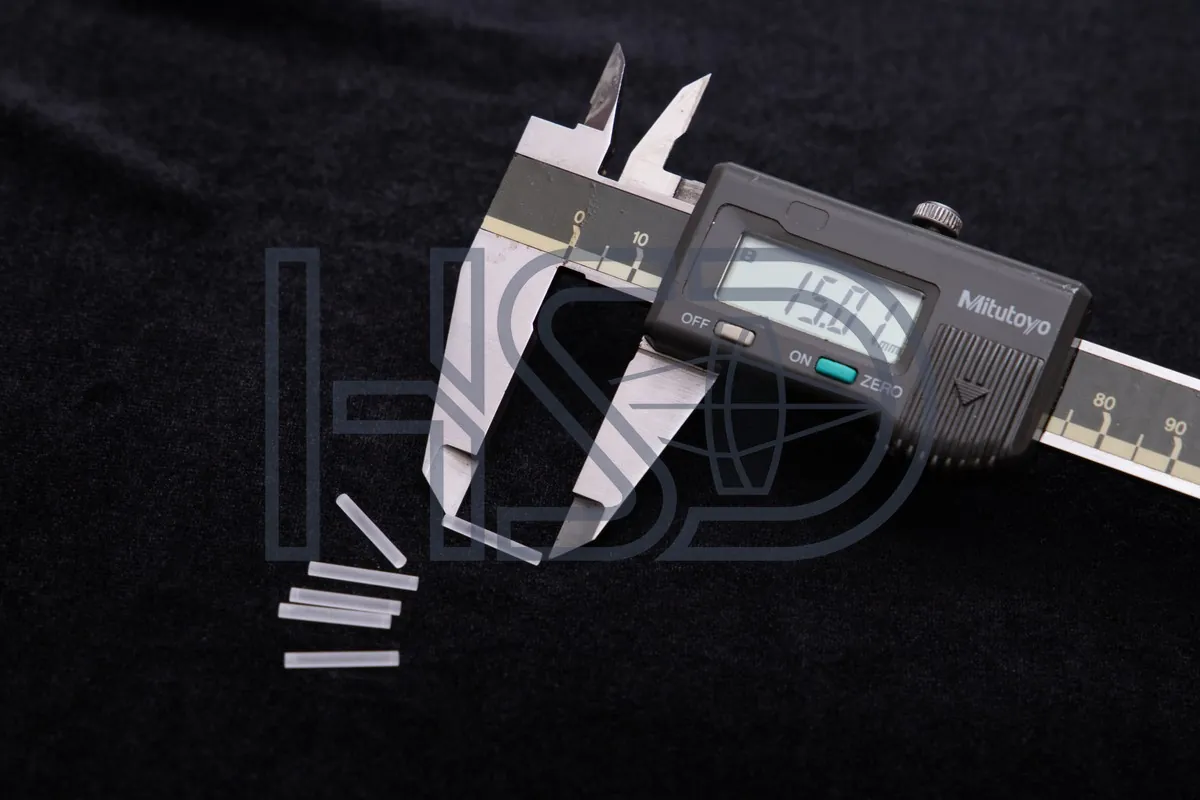
Scope of supply: precision glass rod blanks · laser rod blanks · rod lens blanks for coating labs — uncoated, made to your drawing.
| Item | Specification |
|---|---|
| Rod lens diameter range | Φ1.19–8.0 mm; lengths up to 46 mm (per drawing) |
| Diameter tolerance | −0.02 / −0.04 mm (fit) |
| Centration | ≤3′, tighter per drawing |
| Surface quality | 40/20 · MIL-PRF-13830B / ISO 10110-7 5/40-20 |
| Edge chipping | ≤0.05 mm, per drawing · ISO 10110-7 E 0.05 |
| Coating | BBAR 400–700 nm, R<0.5% (per drawing) |
| Glass | Per drawing: JGS1 / H-ZF / H-LAK / H-K9L / N-SK15; material certificates with each batch |
| Length tolerance | Per drawing |
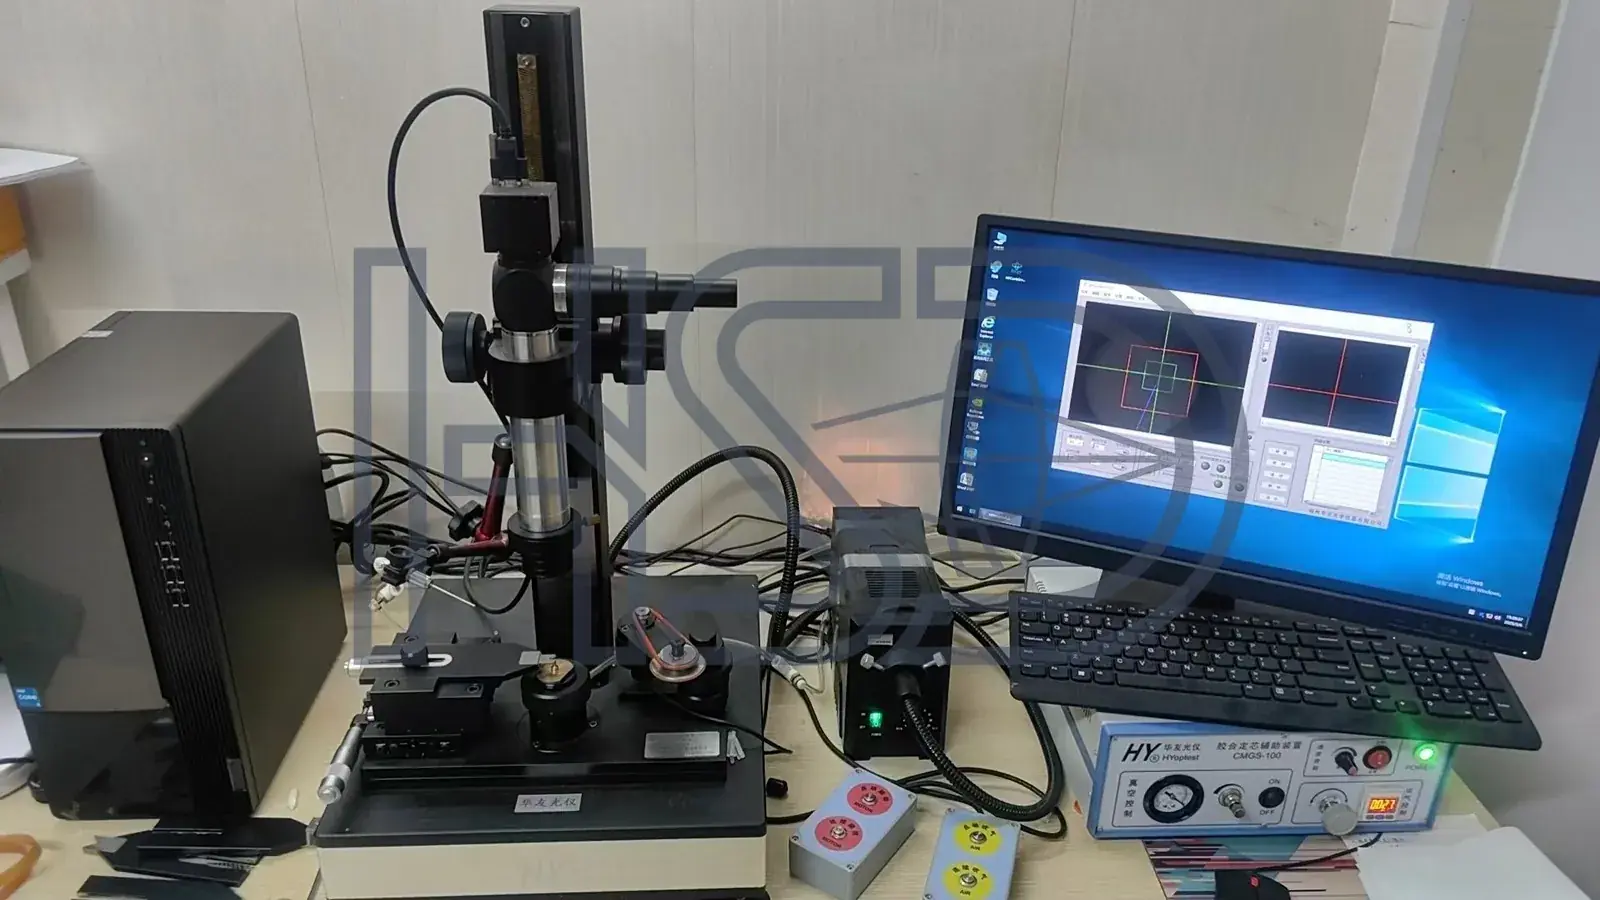
Centration is measured per ISO 10110-6 (≤3′, tighter per drawing) and the measured value goes on the COA — not a "within spec" line. Photo: our inspection bench.
You send the drawing, we make the rod lenses — NDA protected, MOQ 10. If we can't do it, we'll tell you why.
Send Your Drawing →Email [email protected]Application context
This page covers precision glass rod blanks, Φ1.19–8.0 mm, supplied uncoated for coating labs with material certificate.
Check on the drawing: diameter, length, material grade and end condition.
A blank is uncoated and made for the coating lab; we hold the same diameter tolerance and COA process.
Inspection & Metrology
Every batch is verified with interferometry, centration measurement and surface inspection. You get the actual measured values, not a “within spec” checkbox.
Surface form tested by interferometry — PV/RMS values from the actual measurement.
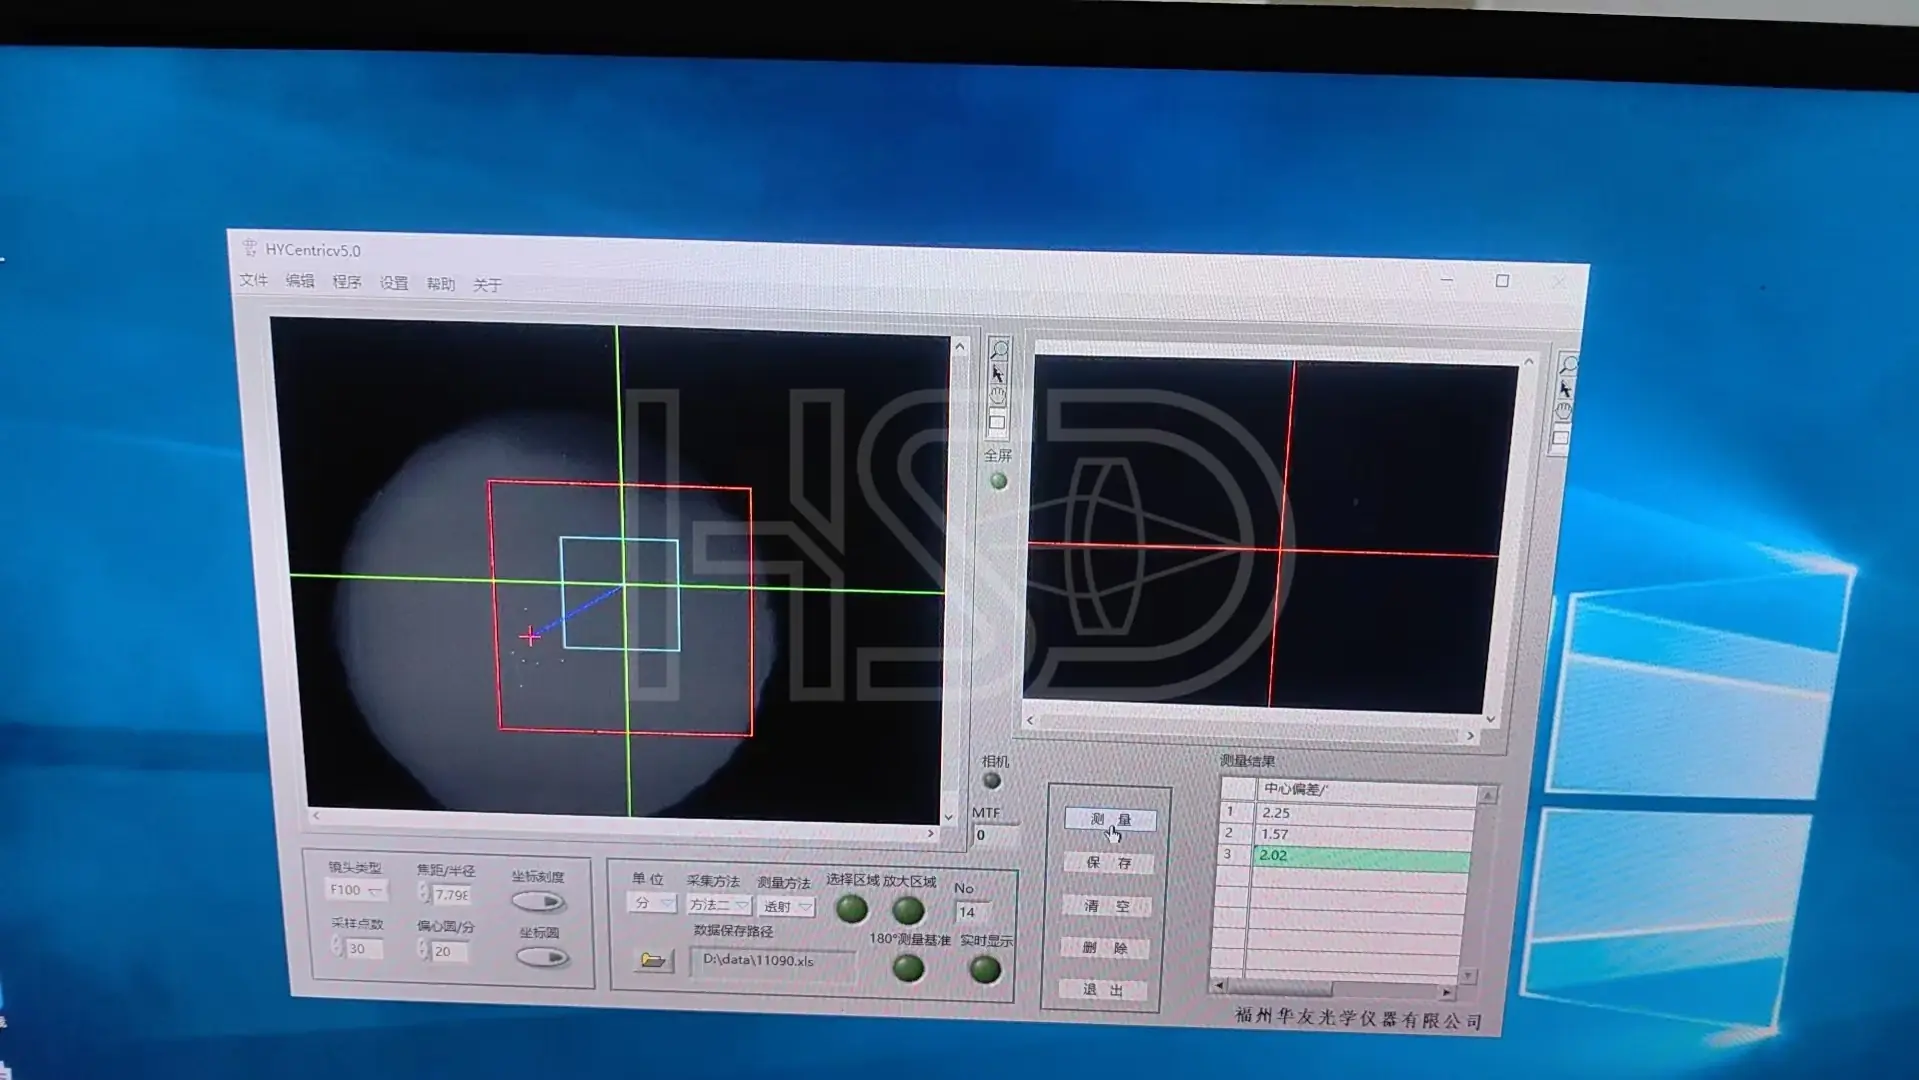
Centration checked on the centration station, typically ≤3′. The reading shown is from a real part — 2.02′.
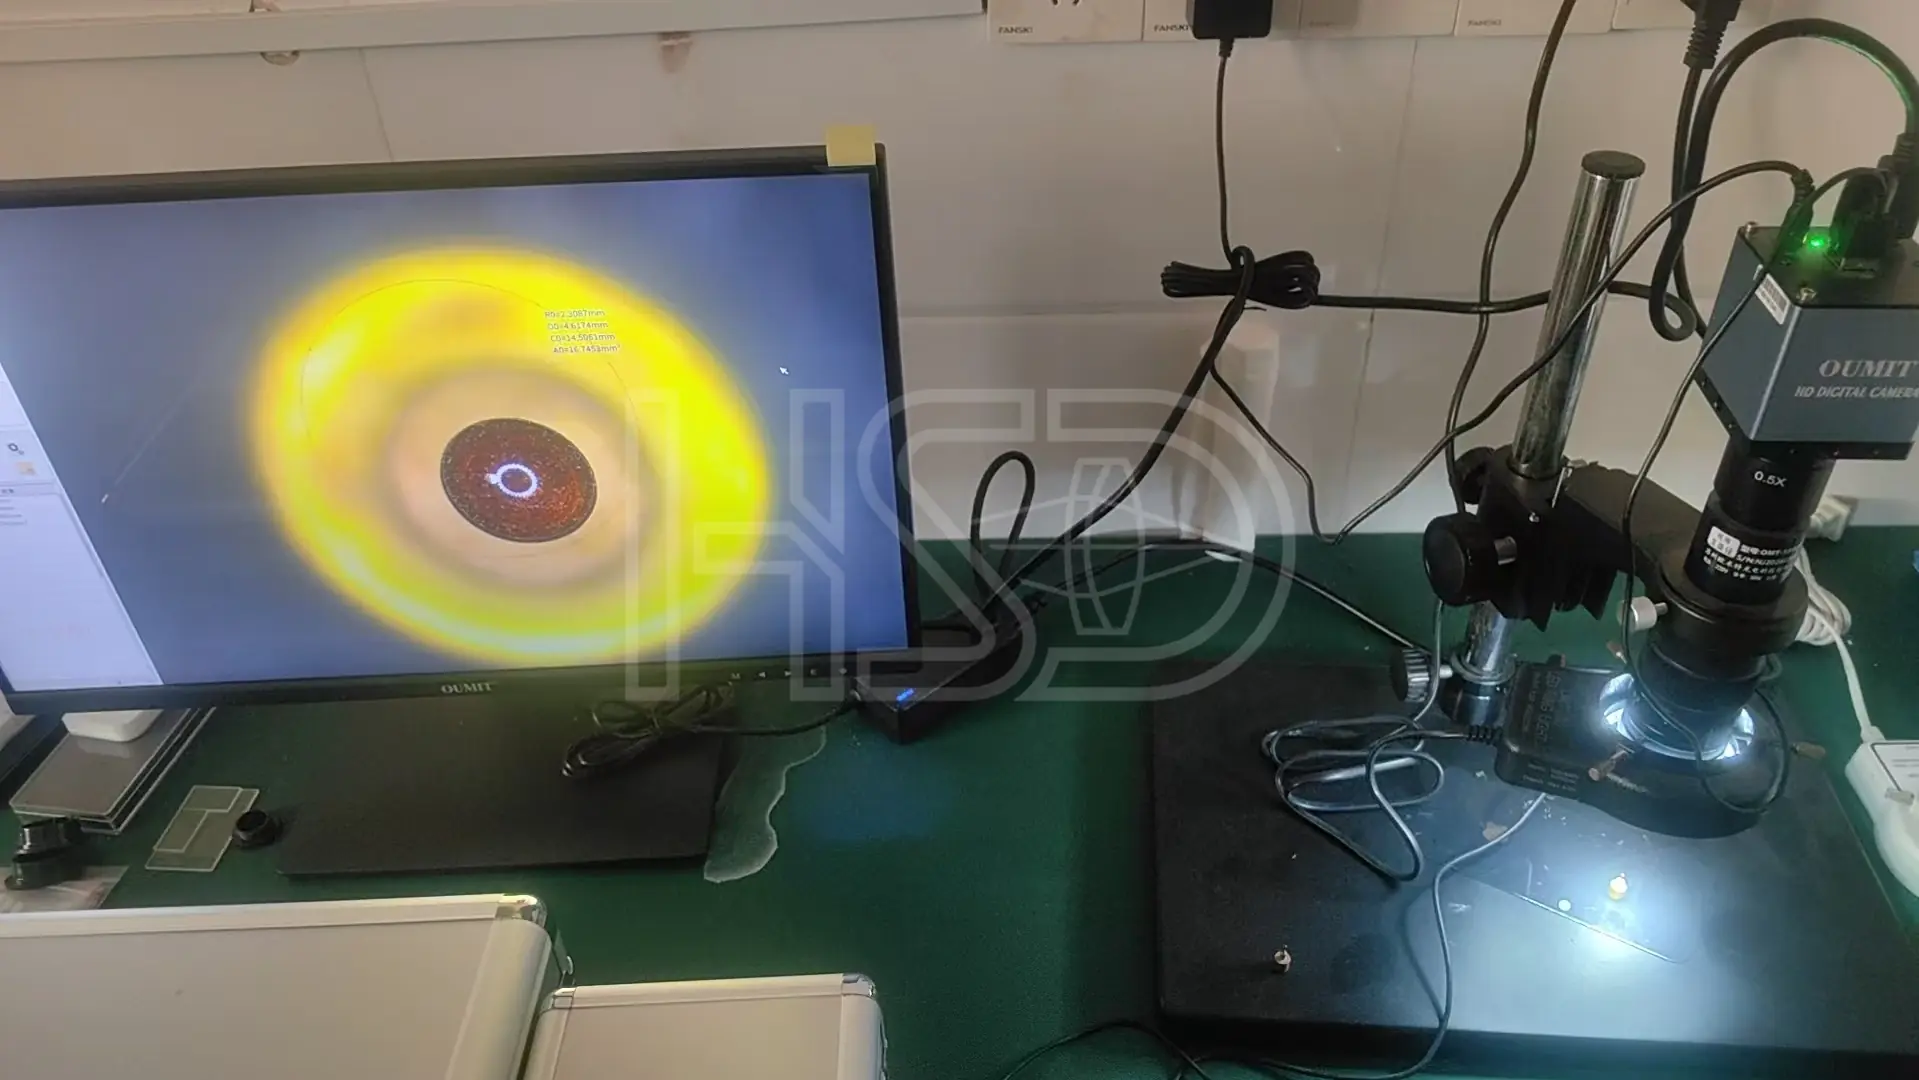
Surface and edge quality inspected under a video microscope — scratch/dig per MIL-PRF-13830B.
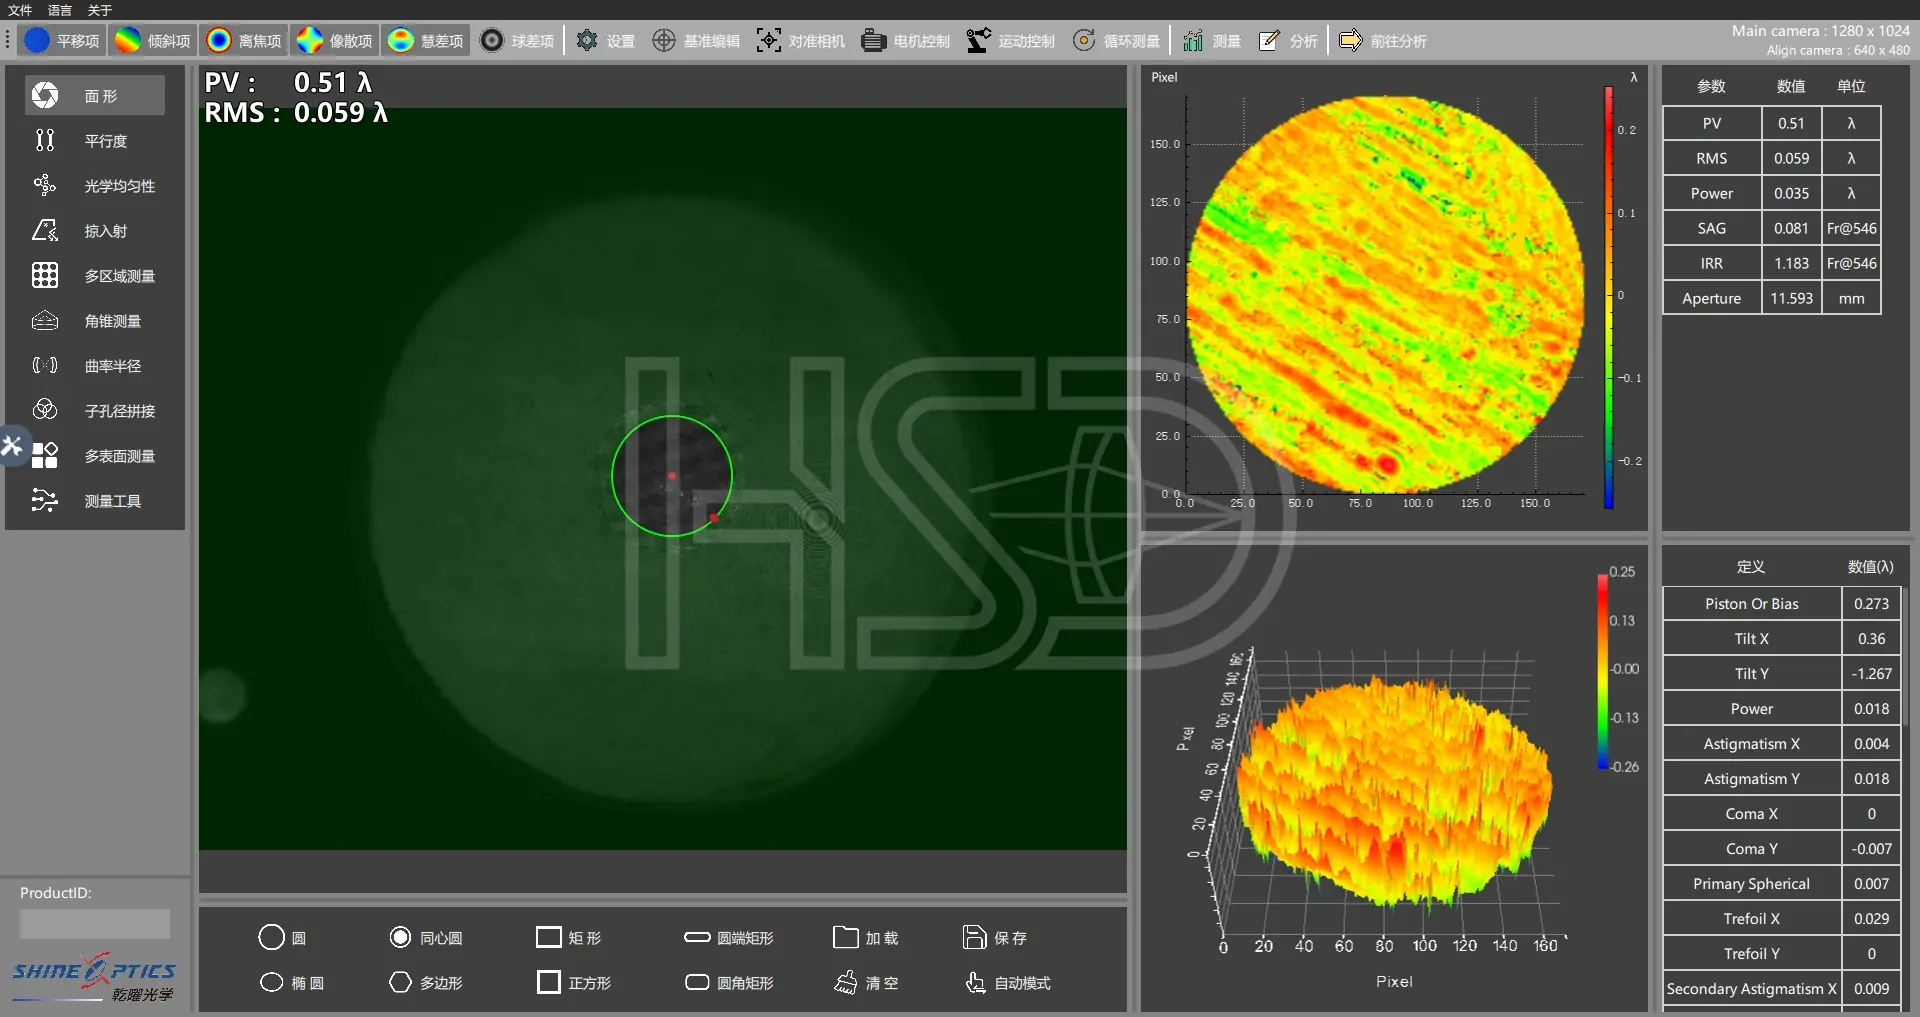
A passing surface from a production run: PV 0.51λ, RMS 0.059λ. Rejects never leave the workshop.
Measured COA per batch — ask for a sample COA with your quote. · Learn how to read a surface map →
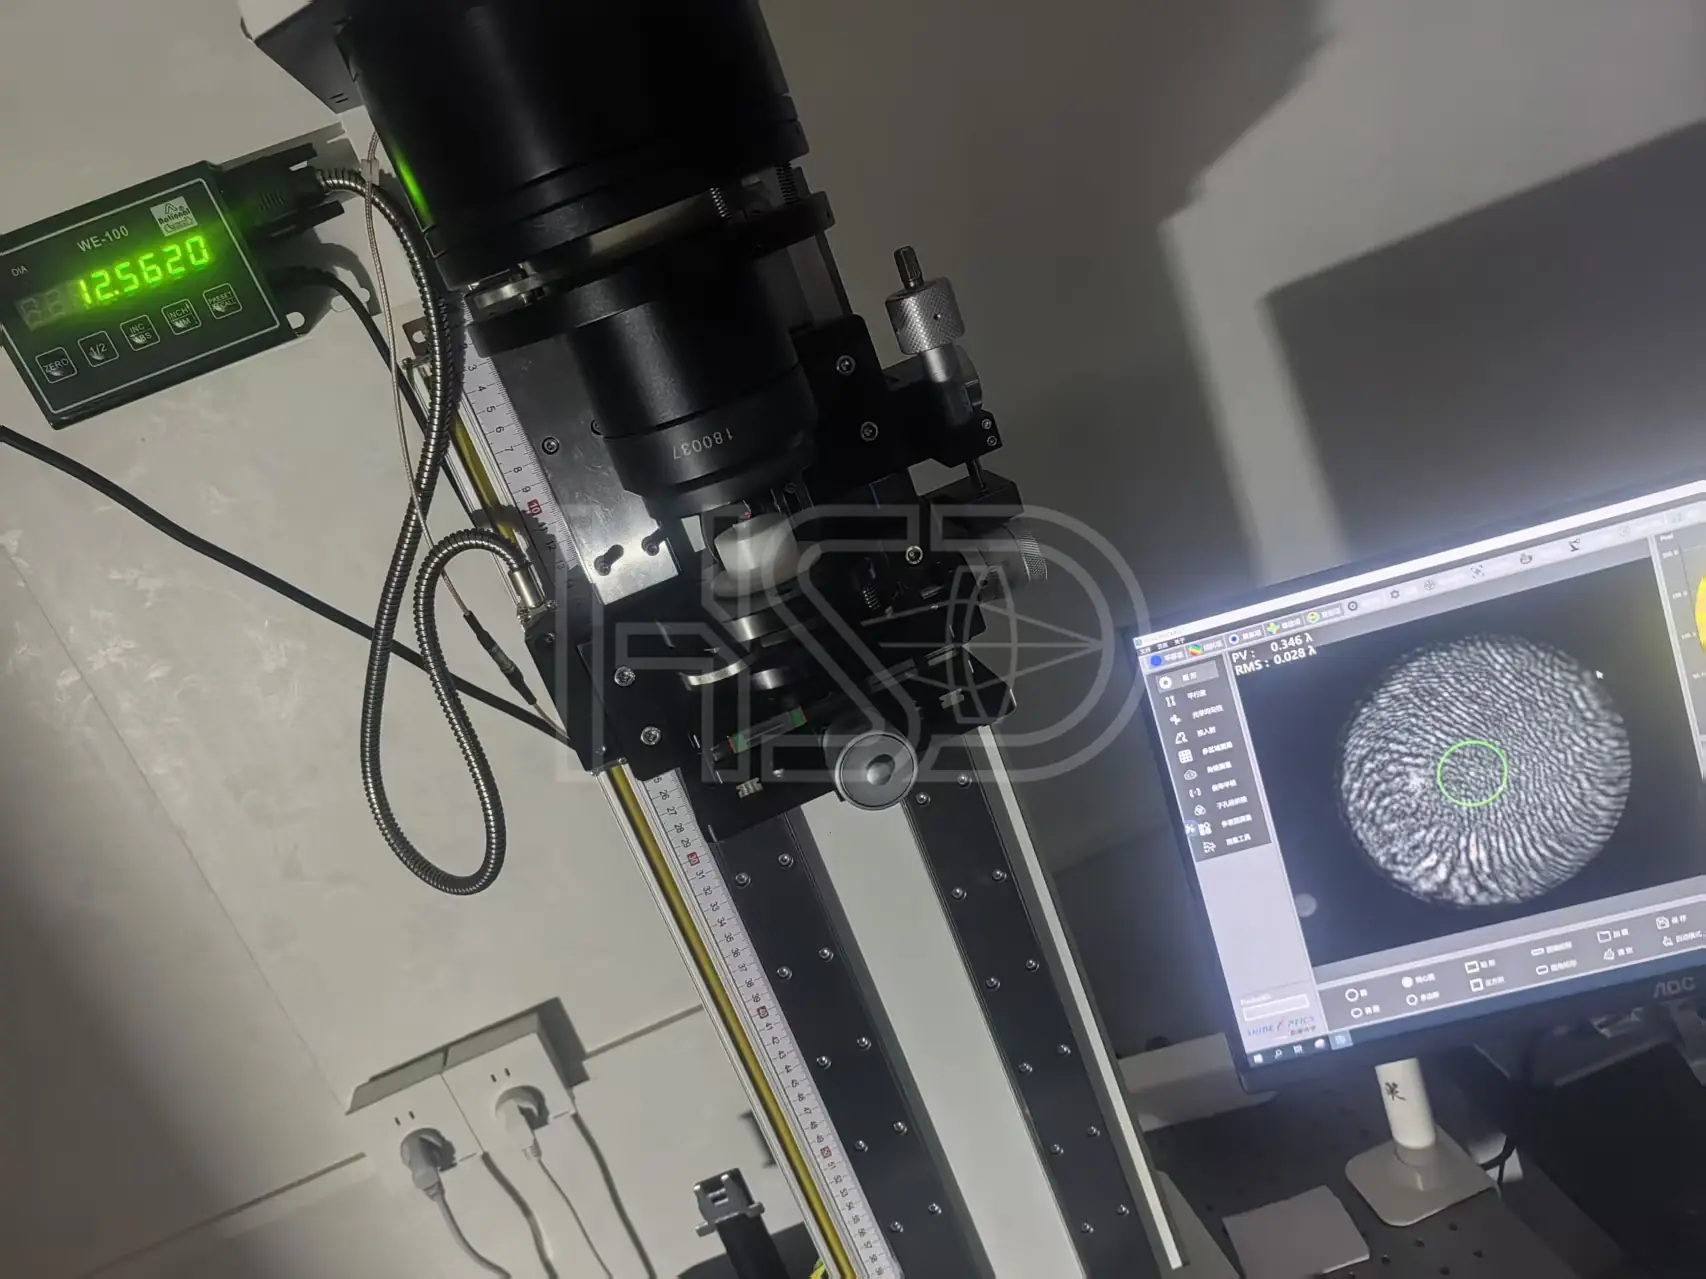
Waviness record on an uncoated blank — PV 0.346λ.
Real measurement, kept on file. Your COA gets the same kind of data.
Watch rod lens grinding, polishing, centration measurement and final inspection in real time. All information shared during the tour is confidential — your NDA is welcome.
Schedule a Live Video Tour